Isolator FAT and SAT: What to Check Before Shipment and on Site
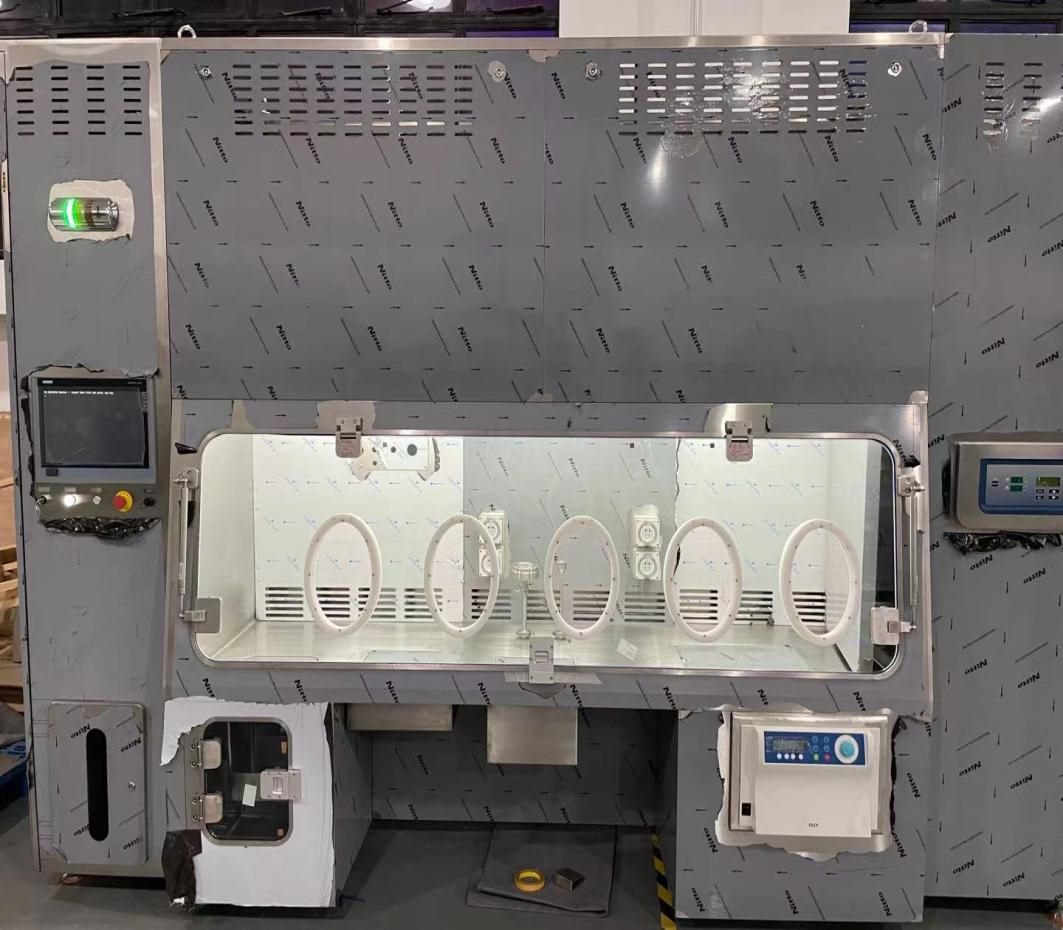
The factory acceptance test is the last chance to find problems while the isolator is still in the manufacturer’s workshop, where fixing them is quick and cheap. This guide sets out what an isolator FAT and SAT should cover, how they connect to qualification, and a practical checklist you can adapt.
- FAT proves the isolator meets the URS before it leaves the factory; SAT proves it still does after transport and installation.
- Agree the FAT protocol and acceptance criteria in advance, traced to URS requirements.
- Test what can break or drift in transport again at SAT: leak rate, HEPA integrity, airflow, sensors and interlocks.
- Well-documented FAT results can be leveraged in IQ/OQ, which shortens site work — if the test conditions are representative.
- Bring the people who will run the isolator to the FAT: ergonomics and operating problems are cheapest to fix there.
Where FAT and SAT fit
An isolator project moves from requirements to a qualified, working system through a chain of documents and tests. Factory acceptance (FAT) and site acceptance (SAT) are the two commissioning tests that sit between design and formal qualification.
- FAT is carried out at the manufacturer, with the isolator fully assembled and running on temporary utilities. It verifies that what was built matches the approved design and the URS.
- SAT is carried out after installation at the user’s site, connected to the real utilities and building. It verifies that nothing was damaged or changed in transport and that the isolator works in its final environment.
EU GMP Annex 15 allows FAT results to be used in qualification if it is shown that the function is not affected by transport and installation. Done properly, this avoids repeating long tests on site.
Before the FAT
- Protocol approved in advance. Each test traced to a URS requirement, with method, instrument and acceptance criterion stated.
- Calibrated instruments. Certificates for particle counters, anemometers, pressure and H₂O₂ sensors, and the leak test instrument.
- Documents ready for review. Drawings, P&IDs, material certificates, weld records, filter certificates, software design and the draft manuals.
- The right people. QA and validation, and also operators and maintenance staff. A mock-up review of glove port positions and reach can be done earlier, but FAT is where everyone sees the real machine.
Isolator FAT checklist
Adapt the list to the isolator type and the URS. Acceptance criteria come from the URS and the applicable standards.
| Area | What to check |
|---|---|
| Documentation | As-built drawings match the isolator · material certificates (e.g. 316L) · surface finish records · weld documentation · component and filter certificates · software version recorded |
| Construction | Dimensions and layout · surface finish and cleanability, no crevices or dead legs · window and gasket fitting · glove ports, sleeves and gloves as specified · drains and sampling ports |
| Leak tightness | Whole-isolator leak test by pressure decay, result against the specified class (for example ISO 10648-2) · door and transfer port seals · see isolator leak testing |
| Pressure control | Set point reached and held in each operating mode · response to glove withdrawal and door operation · alarm and recovery · see isolator HVAC operating modes |
| Airflow | Air velocity and uniformity at working height for unidirectional zones · airflow visualisation (smoke) of critical zones · air change rate in transfer chambers |
| Filters | HEPA filter installation integrity scan test · filter pressure-drop monitoring |
| Particles | Non-viable particle counts at rest against Grade A (or the specified class) |
| Controls | Every HMI screen and function · user levels and passwords · audit trail and data records where required · recipe handling · printouts or exports |
| Interlocks and alarms | Door interlocks, transfer sequence, simulated alarms (pressure, airflow, filter, H₂O₂, door) and the system response to each |
| Power and utility failure | Behaviour on power loss and recovery · loss of compressed air · safe state and data retention |
| VHP cycle | Complete cycle run: conditioning, gassing, dwell and aeration · concentration, humidity and temperature trends · chemical indicators for distribution · aeration to the specified level and time |
| Ergonomics | Operators perform real tasks through the gloves: reach, visibility, component handling, cleaning access |
Record every deviation in a punch list, agree which must be closed before shipment and which can be closed on site, and sign off the FAT report with that list attached.
Packing and shipping
Transport is where an isolator that passed FAT can be damaged. Check that the packing protects windows and glove ports, that loose parts are labelled against the packing list, that moisture protection is adequate for sea freight, and that shock and tilt indicators are fitted. Note the condition of indicators and packaging on arrival before signing for delivery.
SAT: what to repeat on site
| Test | Why it is repeated |
|---|---|
| Visual inspection and as-installed check | Transport damage, correct position, levelling, connections |
| Utility connections | Real power, compressed air, exhaust and room conditions replace temporary ones |
| Leak test | Seals and joints can move in transport |
| HEPA integrity and airflow | Filters and seals can be disturbed; the room environment affects airflow |
| Sensors and interlocks | Confirm calibration status and function after transport |
| Pressure control in the room | Isolator performance depends on the room pressure and exhaust system |
| VHP cycle | Run in the final environment; the basis for cycle development and the biological indicator studies of PQ |
After SAT
With SAT complete, formal IQ and OQ confirm and document installation and operation, referencing FAT and SAT results where justified. PQ then follows, including VHP cycle qualification with biological indicators — see VHP validation and biological indicators on our main site.
References
EU GMP Annex 15, Qualification and Validation
EU GMP Annex 1 (2022), Manufacture of Sterile Medicinal Products
ISO 10648-2, Containment enclosures — Classification according to leak tightness
ISO 14644-3, Cleanrooms — Test methods
ISPE Baseline Guide Vol. 5: Commissioning and Qualification
Fenggu equipment for this
Aseptic filling isolator
Integrated VHP bio-decontaminates exposed interior surfaces before every campaign; unidirectional airflow, H14 HEPA, pressure and particle monitoring.
View specifications →FG-ISO-STSterility test isolator
Reserved VHP generator port to decontaminate the chamber and exposed surfaces before testing, reducing false positives.
View specifications →FG-ISO-CNNegative pressure isolator
For hazardous materials, where leak tightness and pressure control are central FAT tests.
View specifications →Related application guides: Isolator and RABS decontamination · Cell and gene therapy
Common questions
What is the difference between FAT and SAT for an isolator?
FAT is carried out at the manufacturer before shipment and verifies the isolator against the design and URS. SAT is carried out after installation at the user’s site and confirms that it still meets requirements with real utilities and after transport.
What should an isolator FAT include?
Document review, construction checks, a leak test, pressure control, airflow and HEPA integrity, particle counts at rest, HMI and control functions, interlocks and alarms, power failure behaviour, a full VHP cycle and an ergonomics check with operators.
Can FAT results be used in qualification?
Yes. EU GMP Annex 15 allows FAT results to be used in qualification if it is shown that the tested functions are not affected by transport and installation, and the tests were properly documented.
Which tests should be repeated at SAT?
Those that can be affected by transport or the site environment: visual inspection, utility connections, leak test, HEPA integrity and airflow, sensors and interlocks, pressure control and the VHP cycle.
Who should attend an isolator FAT?
QA and validation staff, engineering, and the operators and maintenance staff who will work with the isolator. Problems with reach, visibility and handling are much cheaper to correct at the factory.
Have a specific space or load in mind?
Send the volume, the materials and what you need to prove. An engineer replies with a recommended setup and what validation will involve.